

What New Freeze-Drying Research Means for Food Production
Mar 25, 2020

Freeze-drying research is moving in several useful directions: changing how energy reaches the food, modifying the material before drying, and adjusting the process using better measurements. The production question is whether an improvement survives a complete comparison: the same food and final requirements, all relevant energy inputs, acceptable product yield, and repeatable operation at the intended load. A shorter laboratory cycle is a reason to investigate, not the whole investment case.
For fruit and vegetable ingredients, the most useful advances will connect process efficiency with the form people actually buy. Whole berries, thin slices and crumble have different acceptance criteria. An energy saving that destroys the required slice shape may be valuable for a different product, but it has not yet solved the original buyer's problem.

Read the experiment before repeating the headline
Start with the material. Identify the crop, cultivar where reported, maturity, preparation, cut dimensions and initial state. A study on a uniform model material can isolate a mechanism very effectively. A study on real fruit adds food variability, but may still use one cultivar and a small, carefully arranged load. Both types of evidence can be useful if the question they answer is kept clear.
Then locate the comparator. Was the new method compared with an optimized conventional process, a fixed reference setting, or a deliberately limited control? Were the products dried to comparable specifications? Were reported savings measured or calculated? Those details determine whether the claim addresses your production problem or a narrower scientific question.
Our freeze-dried fruit range includes different ingredient forms that make this distinction tangible. When assessing a technology for a similar form, use its actual cut and handling requirement as the comparison target. A photograph establishes appearance, while the process record and finished testing establish how that appearance was achieved and whether it is repeatable.
Microwave assistance: faster energy delivery, harder uniformity questions
Microwave-assisted freeze-drying investigates a different route for delivering energy during drying. One important challenge is uneven treatment within the material. Regions may experience different heating histories, so the useful question extends beyond the average temperature or total drying time. Researchers examine how power input and temperature control interact with this nonuniformity.
Kalinke and Kulozik's 2024 study used a model maltodextrin foam rather than pieces of fruit. In their temperature-controlled experiments, higher maximum temperature reduced total energy demand but increased temperature nonuniformity. Differences caused by the tested power range were not statistically significant for energy use or uniformity. This is evidence about a particular controlled experiment, and it shows why a simple higher-power-is-better claim misses the experimental conditions.
A 2025 study by Kalinke and colleagues further examined power and temperature control. Its reported findings describe a trade-off between efficiency and temperature distribution, with targeted control helping balance the two. Read that result as a research direction: a useful next trial should look for unevenly treated regions and the effect of the control strategy on the particular food under consideration.
For a development team, the immediate action is to define what a uniform acceptable result means. Is the concern an under-dried region, loss of shape, darker edges or unacceptable texture? Specify where and how samples will be taken. A favorable whole-batch average can coexist with a troublesome minority of pieces, which may be the part that fails the customer's specification.
Pretreatments: change the starting material as well as the drying behavior
Another research route acts on the food before it enters the freeze dryer. Zhang and colleagues' 2024 strawberry work examined ultrasonic pretreatment, drying characteristics and tissue structure. The reported observations included more uniform tissue structure and accelerated water loss. The finding is specific to the studied strawberry treatment; it is a prompt to evaluate both process behavior and the resulting ingredient, rather than to assume every fruit responds equally.

Ask whether the pretreatment changes the formulation. A physical treatment carried out in water differs from treatment in a solution that can exchange soluble material with the fruit. Record the medium and the material entering and leaving the step. If sugar or other ingredients are introduced, the finished ingredient may have a different composition and product description, even when it dries more quickly.
You also need the resources consumed before the dryer: equipment time, electricity, water, cleaning, transfer and any holding requirement. A shorter freeze-drying stage can be offset by an added operation elsewhere. For a fair technical assessment, preserve the individual measurements as well as the combined result. That makes it possible to see which part of the change deserves further work.
At XMSD, we would first ask where an energy comparison starts and stops. A percentage attached only to the dryer is difficult to use when the proposed method adds a treatment upstream. We prefer a clear process boundary and the mass of acceptable ingredient produced within it. That gives a buyer a meaningful basis for comparing a new sample with an established supply format.
Match the food, the endpoint and the production boundary
Choose the same intended final requirements before comparing methods. These include the agreed moisture-related specifications, appearance, flavor, physical form and preparation behavior where applicable. If one sample is left wetter or more damaged, its lower energy consumption answers a different question. Write the acceptance requirements into the trial plan so they are not relaxed after the most attractive result appears.

Preserve the preparation history. Record whether the food was fresh, previously frozen, blanched, cut or treated in a solution. Our vegetable preparation and freezing guide describes why those upstream steps have their own controls. A freeze-drying comparison should carry forward the relevant history rather than treating all frozen starting material as identical.
Measure the energy boundary that matches the decision. A research question may reasonably focus on one component. A production comparison may include preparation, freezing, drying auxiliaries, defrosting and the energy attributed to cleaning and turnaround. Identify included and excluded items. Where shared equipment serves several processes, document the allocation method rather than implying the meter reads only the tested product.
Keep units precise. Kilowatts describe power; kilowatt-hours describe energy over time. Energy per kilogram also needs a denominator: incoming food, water removed, total dried product or accepted finished product. Each is useful for a different purpose. Use more than one measure when necessary, and avoid comparing figures with different denominators as if they were equivalent.
Keep the precision of the conclusion consistent with the measurement. Record the meter coverage, mass measurement and treatment of missing intervals. If the apparent difference is small compared with the variation between repeated runs, report that uncertainty instead of presenting extra decimal places as proof. A result that remains directionally consistent over representative repeats is more useful for planning than a very precise figure from a single selected run.
Example: a lower subtotal can hide a larger total
Consider a hypothetical comparison producing 10 kg of accepted dried fruit per run. The reference route uses 480 kWh within the agreed preparation-through-drying boundary. A proposed route uses 400 kWh for the existing operations within that boundary and another 100 kWh for an added pretreatment. Its combined energy is 500 kWh. On the same accepted-product basis, the comparison is 48 versus 50 kWh/kg.
The developer initially sees the 400 kWh subtotal and must decide whether it supports an energy-saving claim. The developer instead requests the upstream meter record, adds the 100 kWh and keeps both component and total results. In this illustrative case, the proposed route has a lower subtotal for the existing operations but a higher measured total. It may have another benefit worth testing, yet the complete energy comparison does not support a saving.
The numbers above are invented for explanation, not laboratory findings or XMSD operating data. They demonstrate the accounting method. In a real comparison, also state how startup, standby and turnaround are handled. If only one route includes them, normalize the boundary before using the result to estimate a production cost.
Judge efficiency against accepted product, not just dried mass
A process can remove water successfully while producing more broken pieces than the customer can use. Calculate the mass that meets the intended form requirement after the relevant handling. Keep rejected pieces and any lower-grade material visible in the record. A potential outlet for crumble is commercially interesting, but it should not be silently counted as accepted whole-slice output.

The raspberry crumble format illustrates why accepted yield is application-specific. Small pieces may be suitable for a blend or decoration where whole fruit is unnecessary. For a visible large-piece application, the same size distribution can be a defect. Establish the intended grade and any secondary use before the technology comparison begins.
Example: a favorable batch average changes after sorting
A hypothetical new process uses 300 kWh and produces 12 kg of dried material, which appears to be 25 kWh/kg. After the agreed whole-piece assessment, only 9 kg meets the required grade. Energy per accepted kilogram is therefore 300 divided by 9, or about 33.33 kWh/kg. A reference process using 300 kWh and producing 10 kg of accepted pieces is 30 kWh per accepted kilogram.
The buyer is choosing which process to take into a larger trial. Rather than approving the new route on the 25 kWh/kg headline, the buyer asks the developer to reduce breakage while retaining the energy record and final requirements. The illustrative decision is to continue development, not yet replace the reference process. Any sale of the lower-grade fraction would be recorded separately in the commercial analysis.
A secondary grade can change revenue recovery, but it does not change the mass that meets the original specification. Keep the engineering and commercial views connected without mixing them. Report accepted-grade output, secondary output and disposal separately; then evaluate their actual market values if an investment decision requires that level of detail.
Move from a successful sample to a repeatable run
Scale-up introduces more than a larger starting mass. The arrangement of food, movement between operations, measurement coverage, loading variation and time available for each step may change. Plan intermediate trials that reveal these changes. Preserve enough detail that another operator can repeat the run without relying on the developer's memory or an unusually careful laboratory arrangement.
At XMSD, we would judge a new dried fruit process after the sample has experienced the handling expected in the buyer's application. A tray of intact pieces can become a different ingredient after transfer, mixing and packing. We would compare the usable form at that point with the agreed sample, while keeping a separate record of where the damage appeared. That distinction directs corrective work toward the right operation.

Use independent raw-material lots and repeat runs when assessing robustness. Record the variation rather than selecting the most attractive photograph. If the process works for one narrowly selected lot, state that range of evidence. A promising early result can still justify the next trial, provided the next trial deliberately tests the uncertainty that would matter in routine production.
| Evidence level | What it can support | Next question |
|---|---|---|
| Model-material experiment | A controlled mechanism or parameter comparison | Does the effect persist in the actual food? |
| Small real-food trial | Performance for the tested food and arrangement | What changes with load and raw-material variation? |
| Repeated representative runs | A stronger estimate within the tested operating range | Does the packed product meet intended-use requirements? |
A repeatable run also needs practical recovery rules. Record how interruptions, unusual measurements or a missed target are handled. A development program becomes easier to transfer when the team has documented the unsuccessful run and the corrective decision, not only the final successful settings. The evidence should show the range within which the process has actually been assessed.
Packaging and storage belong in the technology comparison
Carry the accepted sample into the intended package and use pattern. Identify the pack material, fill weight, sealing conditions and storage environment used in the evaluation. A process that changes piece density or fragility can change how the package fills and protects the product. Compare what reaches the user, with the packaging and handling records kept alongside the drying data.

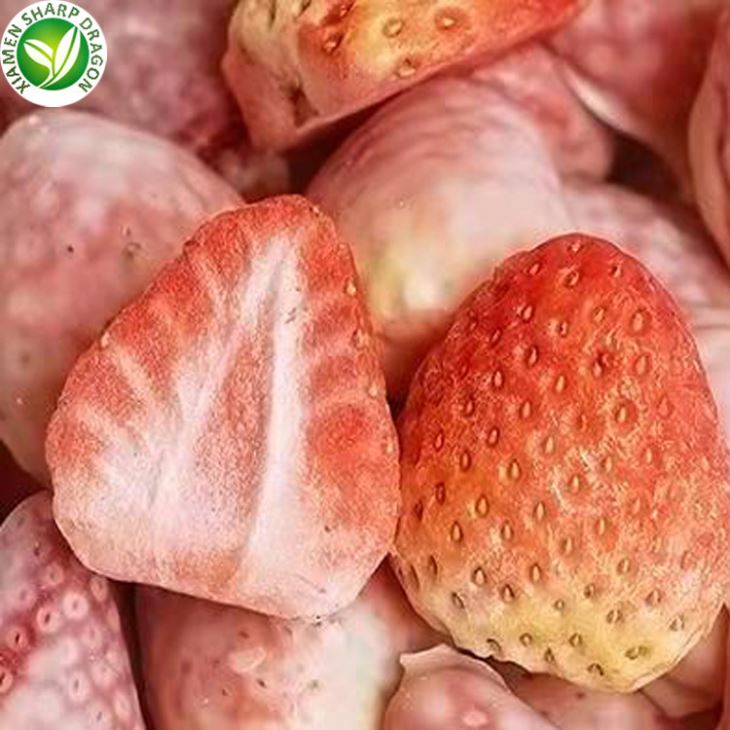
For freeze-dried strawberry ingredients, a buyer may care about an intact topping, a measured portion or performance when mixed into another food. Ask the application team to evaluate the same coded samples that the process team measures. This connects the energy and yield discussion to a result the buyer can recognize, rather than allowing separate teams to approve different versions of the product.
Separate process efficiency, electricity cost and environmental impact. A lower kWh figure within a defined boundary is an energy result. The bill also reflects the applicable tariff and operating pattern.
A broader environmental claim needs an appropriate assessment of the relevant materials, utilities, packaging and losses. Keep the wording as narrow as the supporting measurement when communicating a new result.
Where the next useful advances are likely to matter
The research points toward more informed control rather than a single method that wins for every food. A useful development can be better recognition of uneven treatment, a more suitable pretreatment for one matrix, or a control strategy that maintains the required quality with less energy. The next production step is to test those ideas against the actual ingredient and operating conditions.
Prioritize a development question that can change a decision. If energy is the constraint, establish the complete energy baseline first. If accepted yield is the constraint, map the loss by operation. If inconsistency is the constraint, examine the range of product results and the conditions associated with them. A well-defined question makes a small trial more useful than a broad promise of advanced technology.
Before the next trial, write a short decision statement: which result would justify repeating, enlarging or abandoning this approach? Include both the benefit sought and the quality that must be retained. Share it with the people running and assessing the samples. That small step helps prevent a program from redefining success each time a different measurement looks favorable.
Does a published improvement predict the purchase price?
No. A paper may report a process effect under specified conditions, while a purchase price also reflects raw material, accepted yield, labor, capacity use, maintenance, packaging and commercial terms. Use the research to identify what to test and which records to request. A price comparison still needs a matched product specification and a current quotation.
Is a hybrid process always the better option?
It is a candidate when its additional step solves a defined problem and the complete result supports that choice. Evaluate added resources, changed material properties and operational complexity alongside the benefit. A simpler established process may remain the more practical choice for one product while a hybrid route earns further development for another.
References
- Kalinke and Kulozik, Food and Bioprocess Technology, 2024 - original model-material study of microwave freeze-drying energy and uniformity.
- Kalinke et al., Journal of Food Engineering, 2025 - reported power and temperature-control findings; abstract consulted.
- Zhang et al., Food Chemistry, 2024 - ultrasonic pretreatment and strawberry drying characteristics; abstract-level findings consulted.